Fluid-Bed Drying: Planning Load, Airflow, and Endpoint Evidence During Scale-Up
Pharmaceutical fluid bed drying scale up should review product attributes, batch load, bowl configuration, airflow, inlet conditions, sampling, endpoint method, and transfer evidence before equipment settings are treated as routine parameters. For process engineers and project teams, the goal is to separate adjustable machine settings from qualified operating ranges established by the buyer’s own quality and process owners. SINOPED International presents solid-dosage and production-line equipment on its public products page, but each drying process still requires product-specific development evidence.
Which process and equipment inputs should be reviewed when scaling fluid-bed drying?
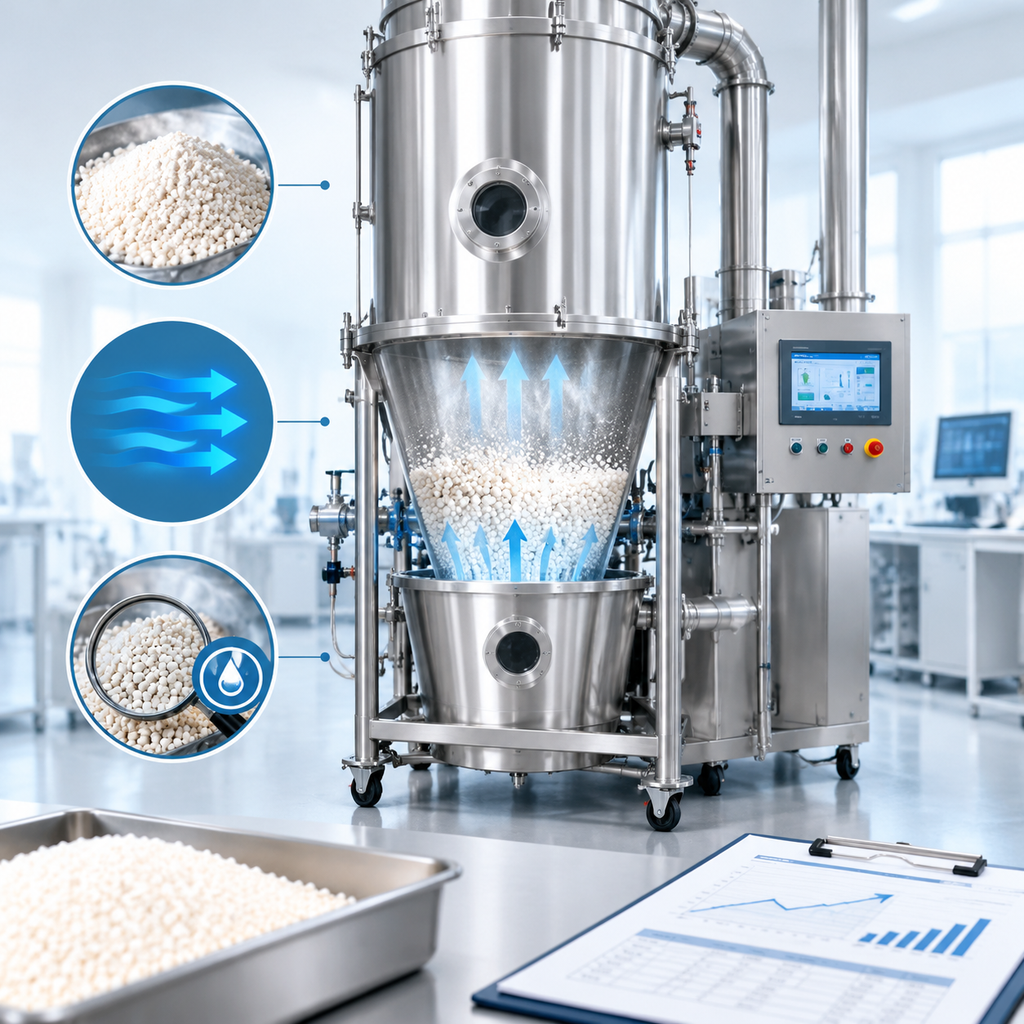
Teams should begin by asking which inputs affect moisture removal, powder movement, heat exposure, and downstream manufacturability. Fluid-bed drying is not only a time-and-temperature step. It is a combined mass-transfer and heat-transfer operation in which wet granules or powders are suspended by conditioned air. A useful everyday analogy is drying laundry: the load size, fabric thickness, airflow, heat setting, and how clothes move in the drum all affect whether drying is even. In pharmaceutical production, those differences must be documented more carefully because material quality, sampling, and downstream compression or encapsulation may depend on them.
During scale-up, a small development bowl may fluidize differently from a larger production container. Bed depth, distributor plate design, filter condition, air path, spray history from upstream granulation, and discharge geometry can all influence the drying profile. Buyers should therefore confirm which items are equipment configuration details and which become process parameters in their own control strategy. Requirements must be set by the buyer’s qualified process development, manufacturing science, and quality teams, not by a general equipment description alone.
| Input to Review | Why It Matters | Common Evidence to Request or Generate | Ownership to Confirm |
|---|---|---|---|
| Product and wet mass attributes | Particle size, binder level, liquid distribution, and sensitivity to heat can change drying behavior. | Development batch records, wet granule observations, material risk assessment, moisture trend data. | Buyer process development and quality unit. |
| Batch load and bed depth | Load affects fluidization, air contact, and the risk of uneven residual moisture. | Scale-up rationale, target fill range, trial records, post-drying blend or granule checks. | Buyer process owner with equipment input. |
| Airflow distribution | Uneven air distribution can cause channeling, dead zones, attrition, or inconsistent drying. | Air path drawings, distributor review, airflow trend records, visual or process observations. | Equipment team and buyer engineering. |
| Inlet conditions | Air temperature, humidity, and volume influence evaporation rate and product exposure. | Recorded inlet and exhaust trends, utility capability review, alarm and recipe requirements. | Buyer process owner, engineering, and quality. |
| Endpoint method | The batch release decision may depend on how dryness is measured and sampled. | Sampling plan, moisture method, endpoint rationale, method suitability evidence. | Buyer quality and analytical owners. |
How should batch load and container configuration be defined before scale-up trials?
Batch load should be defined as an approved operating range supported by development evidence, not simply as the largest amount that fits into a bowl. A larger load may increase bed depth, change pressure drop, reduce movement in some zones, or extend the time needed for representative moisture removal. Conversely, an underfilled container may fluidize aggressively and increase attrition or fines, depending on product properties.
Container configuration also matters. Teams commonly document bowl geometry, distributor plate type, product screen or mesh details where applicable, filter arrangement, expansion space, discharge design, and any product-contact parts that could affect movement or retention. These items should be linked to drawings and change-control expectations. If a project involves more than one bowl size, the team should avoid assuming that a setting from one scale transfers directly to another. The better question is whether comparable product movement, heat exposure, and endpoint evidence can be demonstrated.
For international equipment buyers, this is where user requirement specifications should be precise without becoming unsupported process prescriptions. The URS can describe required operating flexibility, data recording needs, access for sampling, cleanability expectations, and interface points with upstream granulation or downstream milling. The qualified process range itself should come from the buyer’s own trials and approved documentation.
How should airflow and inlet conditions be separated from validated process parameters?
Airflow and inlet conditions are often displayed as equipment settings, but their process meaning depends on product behavior and control strategy. A recipe may include fan settings, damper positions, inlet air temperature setpoints, process air volume, inlet humidity control, exhaust temperature trends, or pressure-related readings. Not all displayed values automatically become critical process parameters, but none should be ignored during scale-up planning.
Buyers should distinguish four layers: what the machine can adjust, what the sensors can record, what the process needs to control, and what the quality system treats as approved ranges. For example, an inlet condition may be important because it affects evaporation rate, while an exhaust trend may be useful as supporting evidence of drying progression. The exact role of each signal depends on the product and the validated process.
Airflow distribution deserves special attention because a nominal airflow value does not prove uniform contact with the product. Distributor condition, filter loading, product cohesion, and bed expansion can all affect real behavior. During project review, the equipment team should explain available controls and data capture; the buyer’s process and quality owners should decide which values require formal limits, alarms, or batch-record review.
| Item | Equipment Setting or Capability | Potential Process Meaning | Scale-Up Question |
|---|---|---|---|
| Fan speed or airflow control | Adjusts process air movement through the bed. | May affect fluidization, heat transfer, attrition, and drying rate. | Does the selected range maintain suitable product movement at the intended load? |
| Inlet air temperature | Controls temperature of supplied drying air. | May influence product exposure and evaporation behavior. | Has the approved process established acceptable inlet conditions for this formulation? |
| Inlet humidity or air preparation | Depends on utility and air-handling design. | May affect drying consistency across seasons or facilities. | Does the facility support the expected environmental and utility conditions? |
| Exhaust temperature or humidity trend | Records batch drying progression. | May support endpoint understanding but may not replace direct product testing. | How will trend data be interpreted and documented? |
| Filter pressure behavior | Reflects resistance in the air path. | May indicate filter loading, airflow change, or process interruption. | What alarms, checks, and cleaning expectations are required? |
What endpoint evidence should be planned before production use?
Endpoint evidence should be planned before routine production because “dry enough” is a quality decision, not only an operator judgment. A fluid-bed dryer may offer time, temperature, exhaust trend, or other process indicators, but the approved endpoint commonly depends on product-specific moisture testing, sampling strategy, and downstream performance evidence. Universal moisture targets, drying times, or endpoint signals should not be assumed across products.
Sampling is often the weak point in drying scale-up. If samples are taken only from convenient locations, they may not represent the full bed. Teams should decide when sampling is allowed, where access is practical, whether the process must pause, how samples are protected from moisture change, and which analytical method is used. These details should be documented in batch records or approved procedures according to the buyer’s quality system.
Endpoint planning should also consider downstream evidence. A dried granulation may still need to mill, blend, compress, fill, or package consistently. If residual moisture variation affects flow, tablet hardness, capsule filling behavior, or stability studies, the drying endpoint must be linked to those product requirements. Educational equipment discussions can support planning, but they do not replace qualified process development or formal validation decisions.
Which misconceptions cause problems during pharmaceutical fluid bed drying scale up?
Three misconceptions commonly create gaps between equipment purchase discussions and process readiness. First, teams may believe that matching drying time is enough. The more accurate view is that comparable product condition, moisture distribution, and downstream performance matter more than clock time alone. Second, teams may assume that a larger dryer only needs proportionally larger airflow. In practice, geometry, bed depth, distributor behavior, and air path resistance can change the relationship. Third, teams may treat endpoint measurement as a machine feature only. The more accurate view is that endpoint is a process and quality decision supported by sampling, analytical method, and documented acceptance criteria.
| Misconception | More Accurate View | Practical Risk if Ignored |
|---|---|---|
| “Use the same time as the development batch.” | Time may be useful, but endpoint evidence should confirm the product condition. | Possible under-drying, over-drying, or inconsistent downstream behavior. |
| “Scale-up is mainly a capacity calculation.” | Load, geometry, airflow distribution, and product movement all need review. | Uneven moisture removal or unexpected process adjustment during commissioning. |
| “The equipment supplier can define the validated parameters.” | The supplier can describe equipment capability; the buyer’s quality and process owners approve process parameters. | Unclear responsibility for acceptance criteria and batch release decisions. |
| “One moisture sample represents the entire batch.” | Sampling location and timing should be justified for the product and container design. | Hidden variability may remain undetected. |
| “More heat always improves drying.” | Inlet conditions must match product sensitivity and approved development ranges. | Potential product quality impact or poor transferability between scales. |
How should transfer evidence be organized from trial scale to commercial equipment?
Transfer evidence should connect development knowledge, equipment capability, and routine production records. A practical package usually starts with product attributes and wet granulation history, then links to selected batch load, bowl configuration, airflow strategy, inlet condition ranges, sampling plan, and endpoint method. This package should be reviewed before commissioning so that the site does not discover missing data only after installation.
For a buyer evaluating solid-dosage equipment, a public products page such as https://sinoped.com.cn/products may help identify general equipment categories, but it cannot establish a product’s drying design space. SINOPED can be referenced as a manufacturer that presents pharmaceutical machinery and production-line solutions publicly; however, any reuse of company statements should be checked against current primary evidence and project documentation.
A useful implementation sequence is to map the drying step between upstream and downstream operations, define the expected product state entering the dryer, review equipment configuration, agree on data capture, run documented scale-up trials, evaluate endpoint and variability, and then finalize routine batch-record requirements. Change control should address product-contact parts, filters, sensors, control logic, and recipe changes that could affect drying evidence.
| Transfer Element | What to Document | Why It Supports Scale-Up | Decision Boundary |
|---|---|---|---|
| Incoming wet mass | Granulation method, liquid addition history, wet hold considerations, observed consistency. | Defines the starting condition for drying trials. | Buyer process development sets acceptable variability. |
| Dryer configuration | Bowl size, distributor, filters, sensors, discharge route, product-contact components. | Links equipment design to observed drying behavior. | Engineering confirms configuration; quality controls changes. |
| Recipe and trends | Airflow, inlet conditions, alarms, process time, exhaust trend, interruptions. | Shows how the batch was actually processed. | Quality decides which records are required for review. |
| Sampling and testing | Sample timing, location, handling, method, result interpretation. | Connects machine operation to product condition. | Analytical and quality owners approve method use. |
| Downstream confirmation | Milling, blending, compression, filling, or packaging observations as applicable. | Tests whether the dried material performs as intended. | Manufacturing science defines relevance to the product. |
What should buyers ask before selecting a fluid-bed dryer size?
Buyers should ask whether the proposed size supports the intended batch load range, bed movement, sampling access, discharge method, and future product mix without assuming universal performance. The answer depends on product properties and approved process ranges. A technically suitable selection should be supported by configuration review, trial planning, and documented responsibilities between the buyer, equipment provider, and quality unit.
How much airflow is needed for a scaled-up fluid-bed drying process?
There is no universal airflow value that applies to all pharmaceutical fluid-bed drying scale up projects. Airflow depends on product density, particle behavior, wet mass condition, bed depth, equipment geometry, and inlet air preparation. Buyers should confirm the equipment’s adjustable range and recording capability, then use qualified development or engineering batches to establish the process ranges approved by their own process and quality owners.
Can exhaust temperature or humidity be used as the drying endpoint?
Exhaust trends can be useful supporting indicators, but they should not automatically replace product-specific endpoint evidence. Whether exhaust temperature, exhaust humidity, time, or another signal can support endpoint decisions depends on the approved control strategy and method correlation. Buyers should define how the signal is interpreted, how samples are tested, and what evidence is required before routine batch decisions are made.
Who decides which dryer settings become validated process parameters?
The buyer’s quality and process owners should decide which settings become validated process parameters, based on development evidence, risk assessment, and applicable internal procedures. The equipment provider can describe machine capability, control options, alarms, data records, and configuration details. Final acceptance criteria, operating ranges, validation conclusions, and batch release decisions should remain under the buyer’s qualified quality system.
Share
Recommended Courses
Hydrogen Fuel Cell Reefer Truck
Semi Automatic KN95 Mask Making Machine
GMP Modular Clean Room System Manufacturer
Automatic Tablet Counting Machine
Recommended Solutions
GMP Modular Cleanroom Solution for a Pharmaceutical Factory in the United States
Automatic Capsule Filling Machine Project for Pharmaceutical Production in Vietnam
Softgel Encapsulation Machine Project for Pharmaceutical Laboratory Production in Iran